A manufacturing plant rarely needs just one industrial chemical. And finding the right chemical for every stage of production is often more complicated than it should be.
Consider an automotive component manufacturer producing machined metal parts.
The process might begin with cutting or machining, where a suitable metalworking fluid is required. Once machining is complete, the components need cleaning to remove residual oil, grease and fine particles.
Depending on the application, they may then undergo surface treatment, coating, assembly or temporary storage. Each stage introduces another requirement: degreasing, rust prevention, phosphating, passivation or precision cleaning.
Now imagine sourcing every chemical from a different supplier.
Different technical teams. Different documentation formats. Different commercial terms. And whenever something goes wrong, multiple suppliers pointing towards one another.
This is one reason manufacturers increasingly value industrial chemical suppliers that understand several stages of the production process.
For businesses searching for an industrial chemical manufacturer with a 100+ product range in India, the real advantage is not simply having access to a long product list. It is finding a manufacturer with the technical capability to supply suitable formulations for different metals, applications and operating conditions.
REFA Chemical Industries Pvt. Ltd., based in Greater Noida, India, develops and manufactures water-based specialty industrial chemicals for metal cleaning, degreasing, surface preparation, metalworking, corrosion protection and other industrial applications.
Its broad product portfolio is designed to address the varied chemical requirements of modern manufacturing industries.
Why Does an Industrial Chemical Manufacturer Need a Large Product Range?
Industrial chemical requirements are rarely identical, even among factories operating in the same industry.
Two automotive component manufacturers may both need an aluminium degreaser. However, their actual requirements can be completely different.
One factory may use a high-pressure spray washing machine to remove machining oil from aluminium die-cast components.
Another may use an ultrasonic cleaning machine to clean precision-machined aluminium parts before assembly.
A third may require a chemical that removes oil without affecting the appearance of an aluminium surface before anodizing.
Although all three applications involve aluminium cleaning, one formulation may not perform equally well in every process.
The differences can arise from:
- Type and amount of contamination
- Metal or alloy composition
- Cleaning equipment and operating temperature
- Required surface finish
- Acceptable residual contamination
- Rinsing and drying arrangements
- Downstream manufacturing operations
- Customer-specific quality requirements
This is why a technically developed industrial chemical portfolio includes multiple formulations rather than relying on a single universal cleaner.
A large product range becomes valuable when it represents meaningful differences in chemistry, application and performance not merely different product codes.
REFA Chemical Industries: A Multi-Product Industrial Chemical Manufacturer in India
REFA Chemical Industries Pvt. Ltd. is an Indian specialty chemical manufacturer with its manufacturing facility in Greater Noida, Uttar Pradesh, and its corporate and marketing office in Noida.
The company focuses on water-based industrial chemical formulations for manufacturing operations, particularly metal processing, cleaning and surface treatment.
REFA’s industrial portfolio covers multiple chemical categories, including metal degreasing, precision cleaning, metal pretreatment, phosphating, passivation, rust removal, corrosion prevention, metalworking fluids and industrial maintenance.
Its products serve manufacturers working with aluminium, stainless steel, mild steel, cast iron, copper, brass and other industrial materials.
For industrial buyers, this means the company can be considered for multiple chemical requirements across the production process, rather than only one isolated application.
The exact chemical grade, working concentration and operating conditions depend on the application and should be established through technical evaluation.
Understanding REFA’s Industrial Chemical Product Range
A broad industrial chemical portfolio is best understood by looking at the manufacturing problems each product category addresses.
1. Industrial Metal Cleaning and Degreasing Chemicals
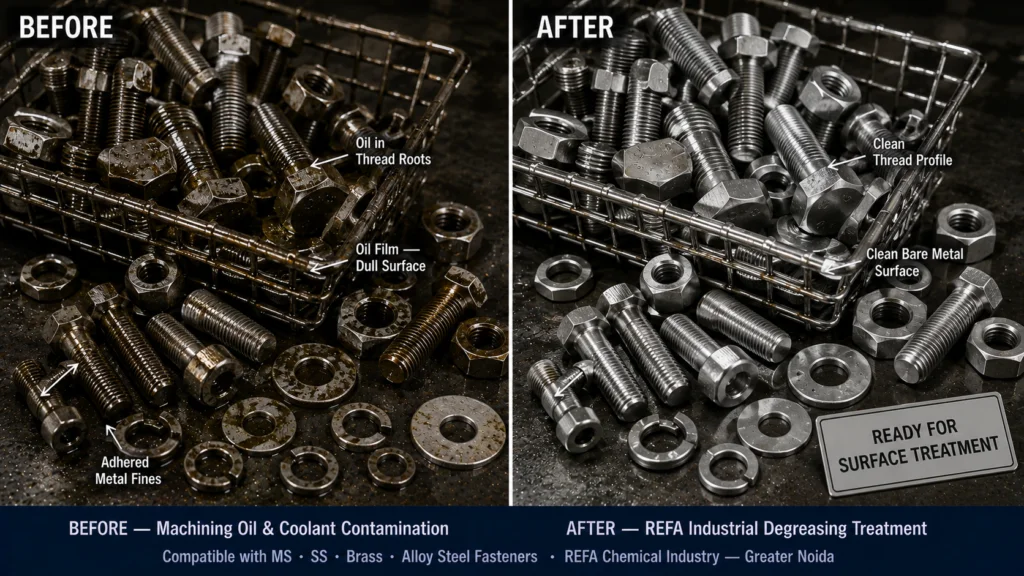
Metal cleaning is one of the most important steps in industrial manufacturing.
Machining, pressing, fabrication and handling can leave oils, grease, carbonaceous residues, polishing compounds and other contaminants on component surfaces.
If these contaminants are not removed adequately, they may interfere with painting, coating, welding, assembly or inspection.
REFA’s metal cleaning and degreasing portfolio includes formulations for different substrates and cleaning requirements.
Major application categories include:
- Aluminium and aluminium die-cast component cleaners
- Mild steel and cast iron degreasers
- Stainless steel cleaning chemicals
- Copper and brass cleaning formulations
- Multi-metal cleaning chemicals
- Heavy-duty industrial oil and grease removers
- Application-specific immersion and spray cleaners
Chemical selection must consider both cleaning efficiency and material compatibility.
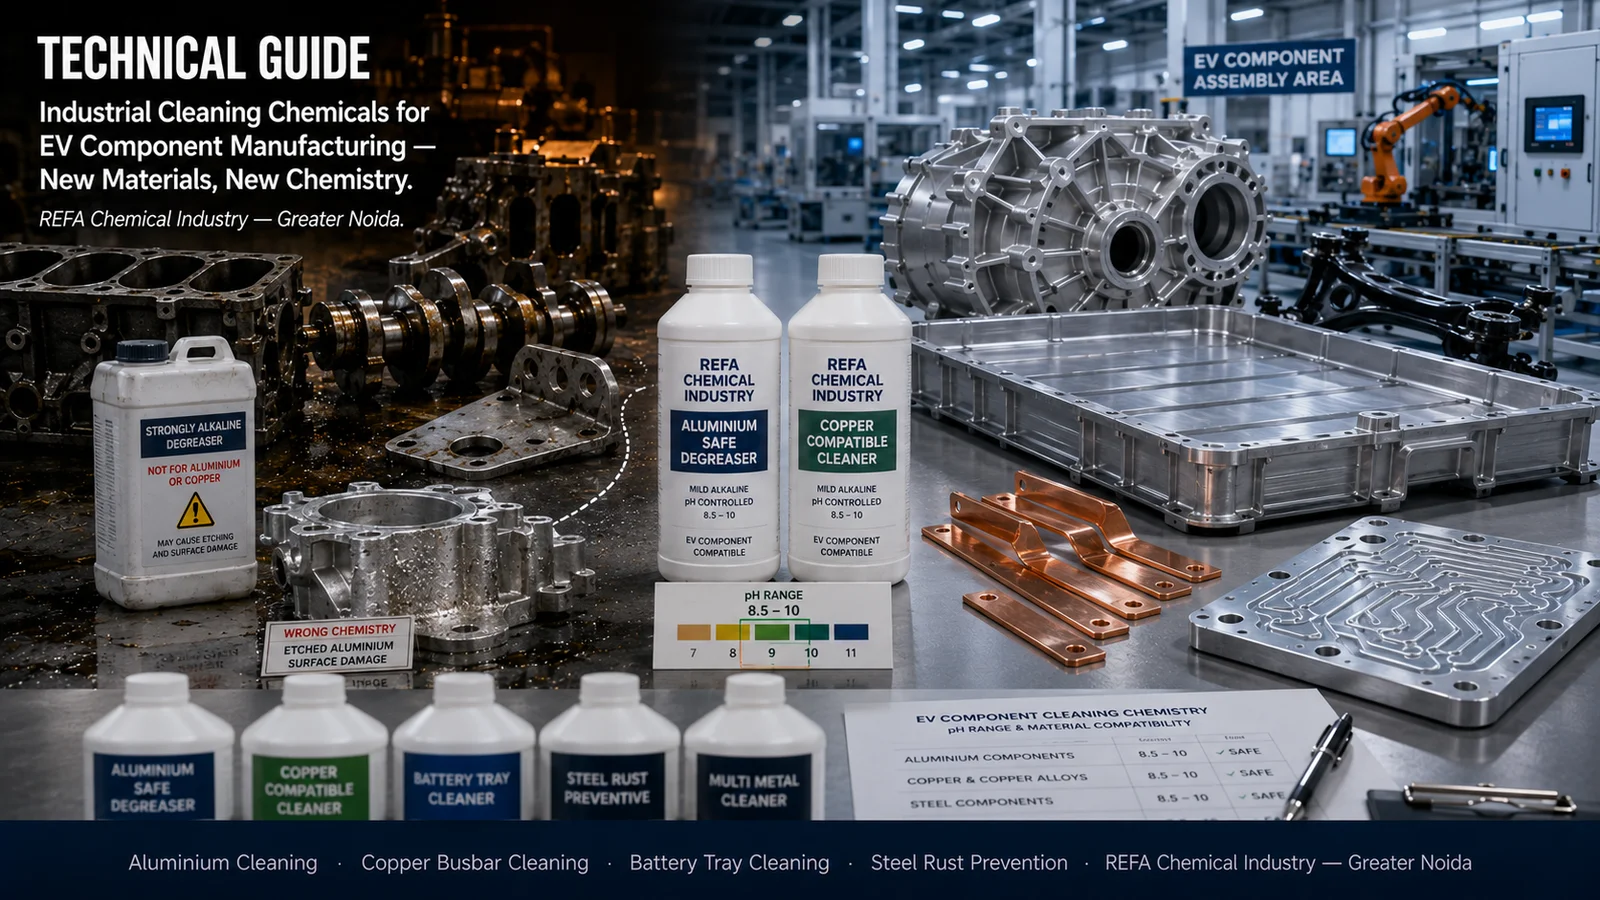
For example, a highly alkaline cleaner may remove heavy oil effectively from certain steel components but may not be appropriate for sensitive aluminium surfaces without suitable formulation controls.
The objective is to remove contamination while preserving the required condition of the component.
2. Precision Cleaning and Ultrasonic Cleaning Chemicals
Not all components are considered clean simply because they look clean.
In automotive, hydraulic, HVAC and precision engineering applications, residual particles and contaminants can affect component performance.
A machined component may appear visually spotless but still contain fine metallic particles inside holes, channels or complex geometries.
Precision cleaning processes are designed to achieve defined cleanliness requirements.
REFA offers water-based cleaning chemistry for applications involving ultrasonic cleaning, immersion cleaning, spray washing and other industrial component washing methods.
Suitable formulations are selected according to factors such as contaminant type, substrate, operating conditions, rinsability and the required cleanliness standard.
Where applicable, manufacturers may evaluate particulate cleanliness using methods associated with ISO 16232 or VDA 19.1.
However, the cleaning chemical alone does not determine the final cleanliness result. Equipment design, filtration, rinsing, handling and drying are also important.
3. Metal Pretreatment and Phosphating Chemicals
Surface preparation plays a critical role in coating quality and corrosion protection.
Before painting or powder coating, metal components may require degreasing, rinsing, conversion coating and other pretreatment operations.
Poor surface preparation can contribute to coating adhesion problems, premature corrosion and inconsistent finish quality.
REFA’s metal pretreatment chemical categories include:
- Iron phosphating chemicals
- Zinc phosphating chemicals
- Manganese phosphating chemicals
- Cleaner-cum-phosphating formulations
- Surface conditioners and activation chemicals
- Phosphating accelerators and bath maintenance products
- Post-treatment passivation and sealing chemicals
Each treatment has its own application requirements.
Iron phosphating, for example, is commonly associated with selected paint pretreatment applications, while zinc phosphating may be selected where more demanding coating and corrosion-resistance requirements apply.
Manganese phosphating is used in certain engineering applications where its functional surface characteristics are required.
The correct process depends on the component, coating system, service environment and applicable customer specifications.
4. Rust Removal and Corrosion Prevention Chemicals
Corrosion can become a costly problem long before a component reaches its customer.
Steel parts may develop surface rust during storage, movement between manufacturing stages or transportation.
REFA’s rust treatment and corrosion protection categories address applications such as:
- Removal of surface rust from ferrous components
- Chemical treatment of oxidised metal surfaces
- Temporary rust prevention during storage
- Corrosion protection between manufacturing operations
- Post-cleaning protection of susceptible components
Rust removal and rust prevention serve different purposes.
A rust remover treats existing corrosion or oxide deposits, whereas a rust preventive is intended to reduce the likelihood of corrosion forming during a defined period or exposure condition.
Manufacturers should select products according to metal type, storage conditions, required protection period and downstream process compatibility.
5. Metalworking Fluids and Lubricants
Metalworking chemicals are involved in many manufacturing operations before a component reaches the cleaning stage.
Cutting, drawing, stamping and forming processes create friction and heat and require appropriate lubrication.
REFA’s metalworking chemical categories include cutting fluids, drawing lubricants, stamping fluids and related process formulations.
A suitable metalworking fluid must be evaluated for the particular operation, material and equipment.
It is also important to consider what happens after machining.
A fluid that performs well during production but is difficult to remove during component cleaning may create additional costs.
This is where a manufacturer familiar with both metalworking and cleaning chemistry can offer practical value.
6. Aluminium Surface Treatment Chemicals
Aluminium is widely used in automotive components, cookware, electrical products and engineering applications.
However, aluminium surfaces can react differently from steel when exposed to unsuitable chemicals.
The formulation and process conditions must be selected carefully to avoid unwanted staining, excessive etching or surface damage.
REFA’s aluminium-related chemical categories include cleaning, degreasing, brightening, etching and selected surface preparation applications.
Chemical selection depends on the alloy, initial surface condition and desired finish.
A product intended for heavy-duty aluminium degreasing should not automatically be used for precision cleaning or cosmetic surface preparation.
7. Vibratory Cleaning and Finishing Chemicals
Vibratory finishing equipment is used in selected metalworking industries for cleaning, deburring, burnishing and surface finishing operations.
The process may combine mechanical media action with an appropriate chemical compound.
REFA’s vibratory chemical range covers applications involving aluminium, steel, stainless steel, copper, brass and other compatible materials.
The chemical compound is only one part of the process.
Media selection, machine operating conditions, component geometry and the desired surface finish must also be considered.
8. Industrial Maintenance and Specialty Cleaning Chemicals
Manufacturing facilities also require chemicals for maintenance and cleaning outside the main production line.
Industrial floors, machine exteriors, bins, equipment and selected plastic components may require different cleaning approaches.
REFA’s industrial maintenance and specialty cleaning portfolio addresses several of these requirements.
The correct product should be chosen according to contamination, surface compatibility, operating conditions and safety requirements.
9. Industrial Water Treatment Chemicals
Water quality affects numerous industrial operations, including cooling systems, process equipment and certain cleaning applications.
REFA’s selected water treatment chemical categories include descaling, scale control, biocides and related maintenance applications.
Such products require application-specific selection, appropriate handling and monitoring of water-system conditions.
Which Industries Benefit From a Manufacturer With a Broad Chemical Portfolio?
A diversified industrial chemical range becomes particularly useful where several chemical processes are involved in the same production facility.
Automotive, Automotive HVAC and Auto Component Manufacturing
Automotive suppliers may require machining fluids, component degreasers, precision cleaning chemicals, pretreatment products and rust preventives.
Different components—such as aluminium housings, steel brackets, hydraulic parts and HVAC assemblies—may require distinct cleaning and surface treatment methods.
A supplier familiar with multiple stages of production can help coordinate chemical selection across departments.
Cookware, Cutlery and Kitchenware Manufacturing
Cookware manufacturers often work with stainless steel and aluminium sheets, pressed components and polished surfaces.
Their chemical requirements can include drawing and stamping lubricants, degreasers, buffing compound removers, surface preparation chemicals and finishing-related products.
Cleaning and finishing quality are particularly important where surface appearance is a major customer requirement.
Aluminium Processing and Fabrication
Aluminium processors require chemical solutions for cleaning, degreasing, brightening and surface preparation.
The correct formulation depends on whether the operation involves sheets, extrusions, tubes, die-cast components or machined parts.
General Engineering and Metal Fabrication
Engineering manufacturers frequently handle several metals and processes under one roof.
They may need metalworking fluids, degreasers, phosphating chemicals, rust removers and corrosion preventives.
Access to a broad product portfolio can simplify supplier evaluation and technical coordination.
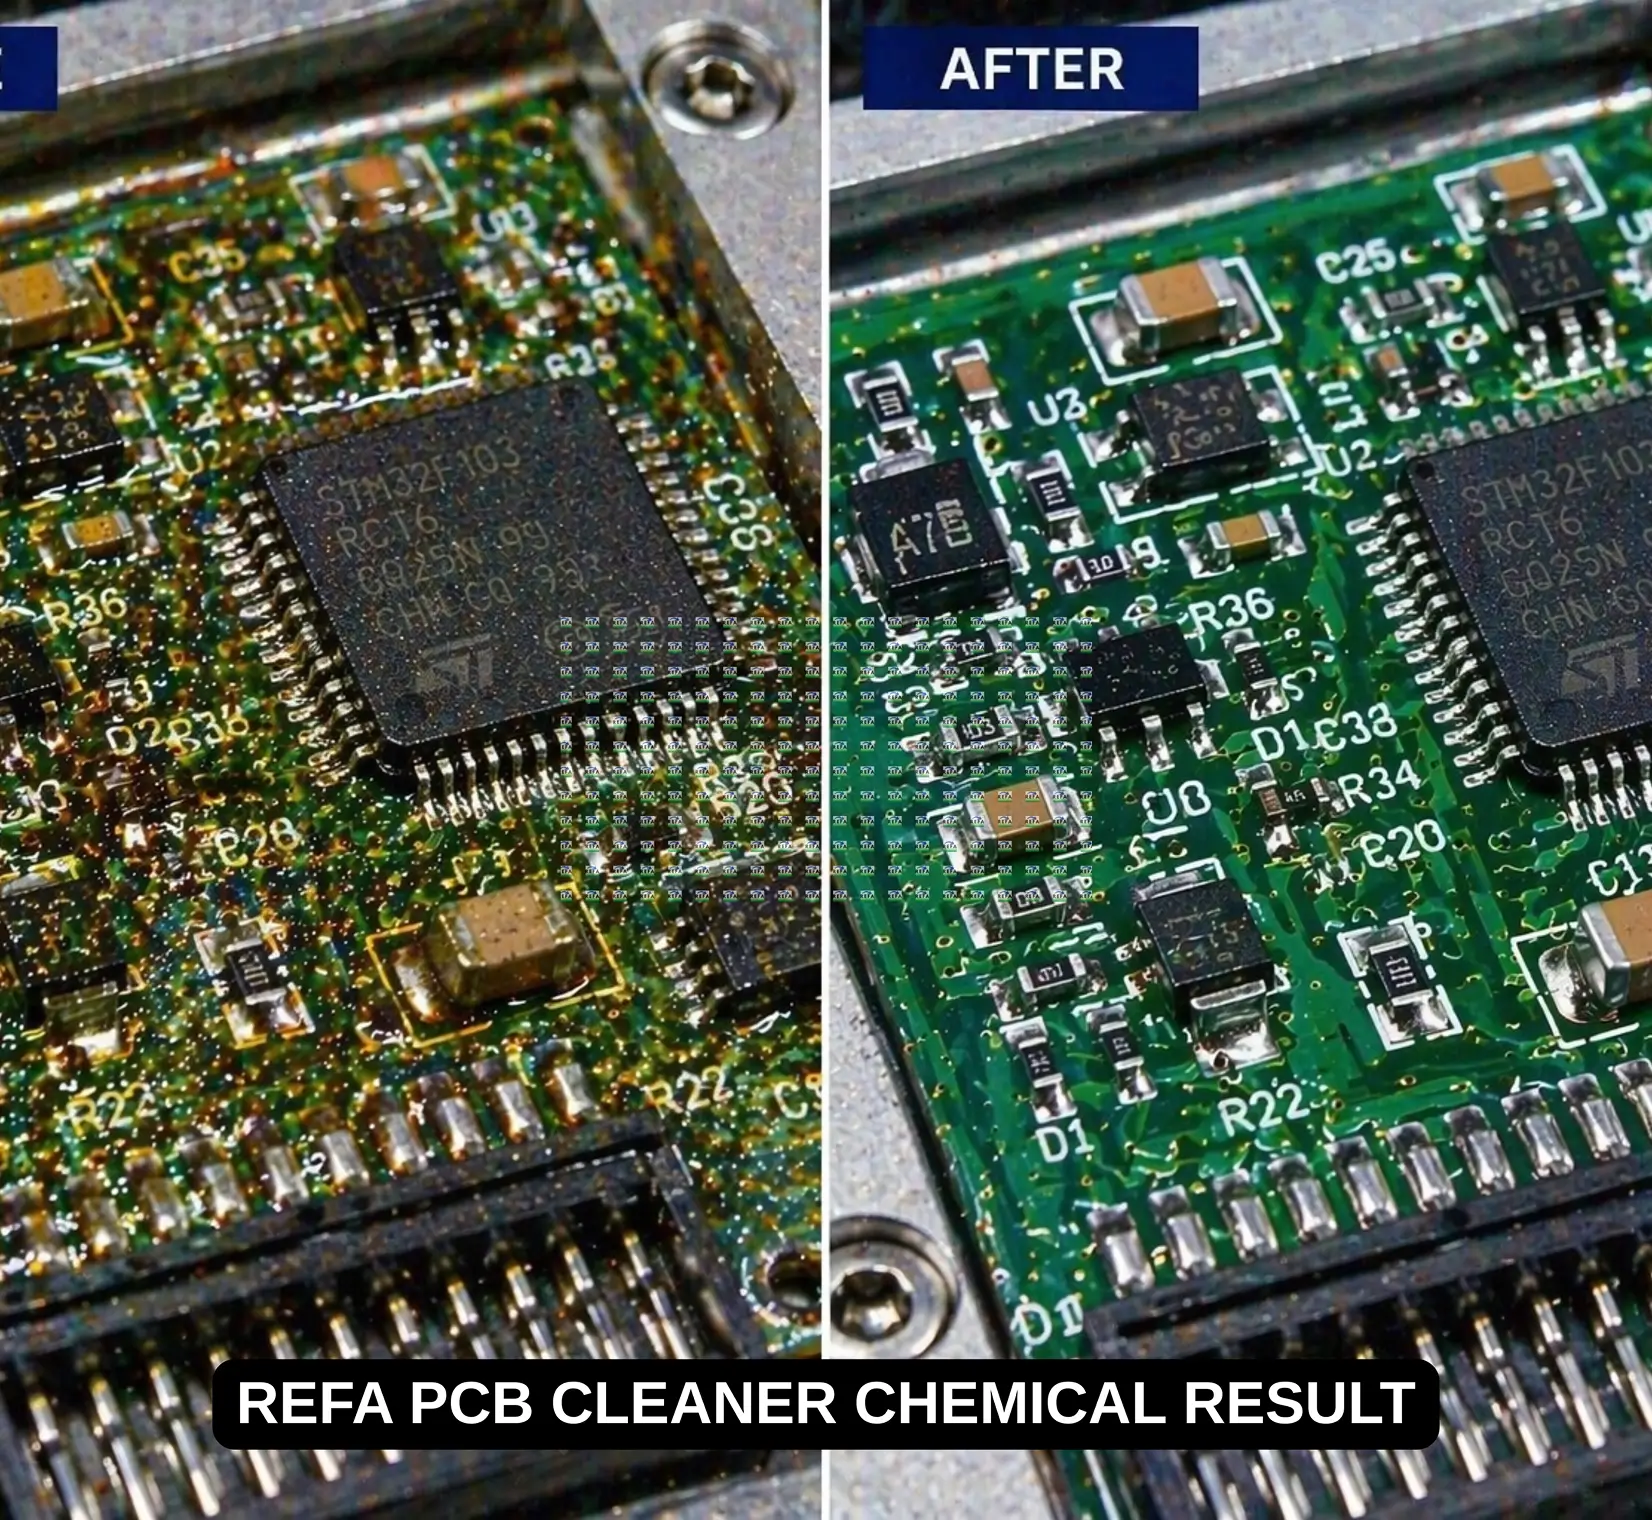
Electronics, PCB and Electrical Manufacturing
Selected electrical and electronics manufacturing applications require specialised cleaning processes.
Chemical compatibility, residue control, rinsing and the relevant cleanliness requirements are particularly important.
Water-based formulations may be suitable for certain applications, but they must be evaluated against the components and process requirements.
Does a 100+ Product Range Mean Better Quality?
Not necessarily.
A chemical manufacturer with 100 or more product grades is not automatically better than a specialist supplying ten well-developed formulations.
The important question is whether the portfolio represents genuine technical capability.
For example, a useful product range might contain different formulations for aluminium, stainless steel, copper, brass and mild steel because each material has different compatibility requirements.
It may also contain separate products for spray, ultrasonic and immersion cleaning because the equipment operates differently.
These distinctions have a technical purpose.
On the other hand, offering many nearly identical formulations without meaningful application differences does not necessarily benefit customers.
When evaluating a manufacturer, industrial buyers should ask:
- Can the supplier explain why one grade is recommended over another?
- Does the company provide appropriate Technical Data Sheets and Safety Data Sheets?
- Can the formulation be tested on actual production components?
- Is the manufacturer able to support process troubleshooting?
- Are product specifications and manufacturing quality consistent?
- Can the supplier recommend alternatives when process conditions change?
The strength of an industrial chemical manufacturer lies in the relevance and reliability of its formulations, not merely the size of its catalogue.
The Advantage of Sourcing Multiple Industrial Chemicals From One Manufacturer
Working with a multi-product industrial chemical manufacturer can offer several practical benefits.
Better Coordination Between Manufacturing Processes
Chemical processes are interconnected.
The lubricant used during machining can affect the cleaning chemical required afterward.
The cleaner used before phosphating can influence surface preparation results.
A manufacturer familiar with these stages can help identify compatibility issues across the process.
Simplified Procurement
Consolidating suitable chemical requirements with fewer suppliers may reduce the administrative work associated with quotations, vendor approvals, documentation and purchasing.
However, procurement teams should still evaluate commercial competitiveness and supply reliability for each product.
More Consistent Technical Communication
When a manufacturing issue involves several chemical stages, having one technical point of contact can make investigation easier.
For example, a coating defect might involve incomplete degreasing, unsuitable rinsing or pretreatment bath conditions.
A supplier with broader process knowledge may be better positioned to investigate the complete sequence.
Opportunities for Application-Specific Formulations
Manufacturers do not always operate under standard conditions.
A factory may have unusual contamination, difficult component geometry or specific customer requirements.
A chemical manufacturer with formulation-development capability may be able to evaluate modifications or recommend a more suitable grade.
Customisation should be validated through technical trials rather than assumed to guarantee a particular result.
Why Water-Based Industrial Chemistry Matters
REFA focuses on water-based industrial chemical manufacturing.
For suitable applications, aqueous formulations can reduce reliance on certain organic solvent cleaning systems and support controlled industrial cleaning operations.
However, water-based does not automatically mean biodegradable, non-toxic or environmentally harmless.
The actual environmental and safety characteristics depend on the ingredients, product concentration, operating conditions and disposal method.
Industrial customers should evaluate chemical safety documentation, wastewater treatment requirements, chemical consumption and total process performance.
The objective is to achieve reliable manufacturing results while managing worker safety and environmental responsibilities.
How to Select an Industrial Chemical Manufacturer in India
Before appointing a supplier for multiple industrial chemical requirements, evaluate the following factors.
Manufacturing capability: Confirm whether the company manufactures the relevant products or operates primarily as a trader.
Product coverage: Identify whether the manufacturer supplies the specific categories needed for your processes.
Technical expertise: Evaluate its understanding of metals, contamination, equipment and downstream operations.
Documentation: Request product-specific SDS, TDS and applicable compliance information.
Trial support: Assess whether products can be evaluated under realistic manufacturing conditions.
Quality management: Review relevant certifications, batch controls and consistency measures.
Commercial reliability: Consider delivery arrangements, lead times, minimum order quantities and after-sales support.
Customisation: Discuss whether application-specific development is possible where standard formulations are unsuitable.
A good industrial chemical manufacturer should be able to explain not only what it sells, but also why a particular formulation is suitable for the customer’s process.
Why Consider REFA Chemical Industries?
REFA Chemical Industries Pvt. Ltd. operates from Greater Noida, one of the industrial manufacturing centres of Delhi NCR.
The company manufactures water-based specialty industrial chemicals for metal cleaning, surface preparation, metalworking, corrosion protection and associated manufacturing applications.
REFA identifies ISO 9001, ISO 14001 and ISO 45001 among its management-system certifications.
Its industrial application focus spans automotive and auto components, cookware and cutlery, aluminium processing, general engineering and other manufacturing sectors.
For businesses seeking an Indian industrial chemical manufacturer with a diversified product portfolio, REFA offers the opportunity to discuss multiple process requirements with a single manufacturer.
The recommended starting point is not simply requesting a catalogue.
It is sharing the manufacturing process, component materials, existing chemicals, operating conditions and quality requirements so that suitable product grades can be shortlisted for evaluation.
Frequently Asked Questions
1. Which industrial chemical manufacturer in India offers a 100+ product range?
REFA Chemical Industries Pvt. Ltd. is a Greater Noida-based manufacturer with a broad portfolio of water-based specialty industrial chemical formulations. Its range covers metal cleaning, degreasing, surface preparation, phosphating, rust prevention, metalworking and other applications.
2. What types of industrial chemicals does REFA manufacture?
REFA manufactures industrial metal cleaners, degreasers, precision cleaning chemicals, pretreatment and phosphating chemicals, rust removers, rust preventives, metalworking fluids and selected industrial maintenance and water treatment chemicals.
3. Where is REFA Chemical Industries located?
REFA’s manufacturing facility is located at Industrial Plot No. A-94, Kasna Ecotech-6, Greater Noida, Uttar Pradesh – 201316, India. Its corporate and marketing office is in Sector 153, Noida.
4. Does REFA manufacture water-based industrial chemicals?
Yes. REFA focuses on water-based specialty industrial chemical formulations for manufacturing applications, including metal cleaning, degreasing and surface preparation.
5. Can one industrial chemical manufacturer supply chemicals for different metals?
Yes. A manufacturer with a diversified portfolio may offer separate formulations for aluminium, stainless steel, mild steel, cast iron, copper, brass and other materials. Product selection must account for metal compatibility and process requirements.
6. Does REFA supply chemicals for automotive component manufacturers?
Yes. REFA serves automotive and auto component manufacturing applications, including metal cleaning, precision cleaning, degreasing, surface preparation and corrosion protection.
7. Can REFA develop customised industrial chemicals?
REFA supports application-oriented chemical formulation development. Customisation depends on the technical requirements, feasibility, validation results and commercial considerations.
8. Does a larger industrial chemical product range reduce procurement costs?
It may simplify procurement and technical coordination, but cost savings are not automatic. Buyers should compare product performance, chemical consumption, supply terms and total operating costs.
9. What documents should an industrial chemical manufacturer provide?
Industrial buyers should request product-specific Technical Data Sheets, Safety Data Sheets and applicable certification or compliance documents. Additional testing or declarations may be needed depending on the industry and application.
10. Does REFA supply industrial chemicals across India?
REFA serves industrial manufacturing customers beyond its Greater Noida location. Availability, delivery terms and commercial arrangements should be confirmed for the required product and destination.
Looking for an Industrial Chemical Manufacturer With a Broad Product Range in India?
Whether your factory requires a metal degreaser, precision cleaning chemical, phosphating solution, rust preventive or metalworking fluid, the most important step is selecting a formulation that matches your manufacturing process.
REFA Chemical Industries Pvt. Ltd. develops and manufactures water-based specialty industrial chemicals for a wide range of industrial applications.
Share your component material, contamination type, manufacturing process and chemical requirements with our team.
We can help identify suitable formulations for technical evaluation and discuss application-specific requirements.
REFA Chemical Industries Pvt. Ltd.
Manufacturing Unit: Industrial Plot No. A-94, Kasna Ecotech-6, Greater Noida, Uttar Pradesh – 201316, India
Email: info@refachemical.com
Website: https://refachemical.com/
REFA — Research Engineered Formulations & Applications.