A manufacturing plant in Pune and a factory in Chennai may be hundreds of kilometres apart, but they can face exactly the same problem: finding an industrial chemical that works consistently and arrives when production needs it.
For many factories, sourcing industrial chemicals is not simply about comparing prices or selecting a supplier from the nearest industrial area.
A metal cleaning chemical that performs well during laboratory testing must deliver consistent results during production. A phosphating chemical must operate within the required process parameters. A rust preventive must provide suitable protection under the actual storage and transportation conditions.
And once the right chemical has been approved, the manufacturer needs dependable supply.
This becomes particularly important for businesses operating multiple manufacturing facilities across India or purchasing industrial chemicals from overseas.
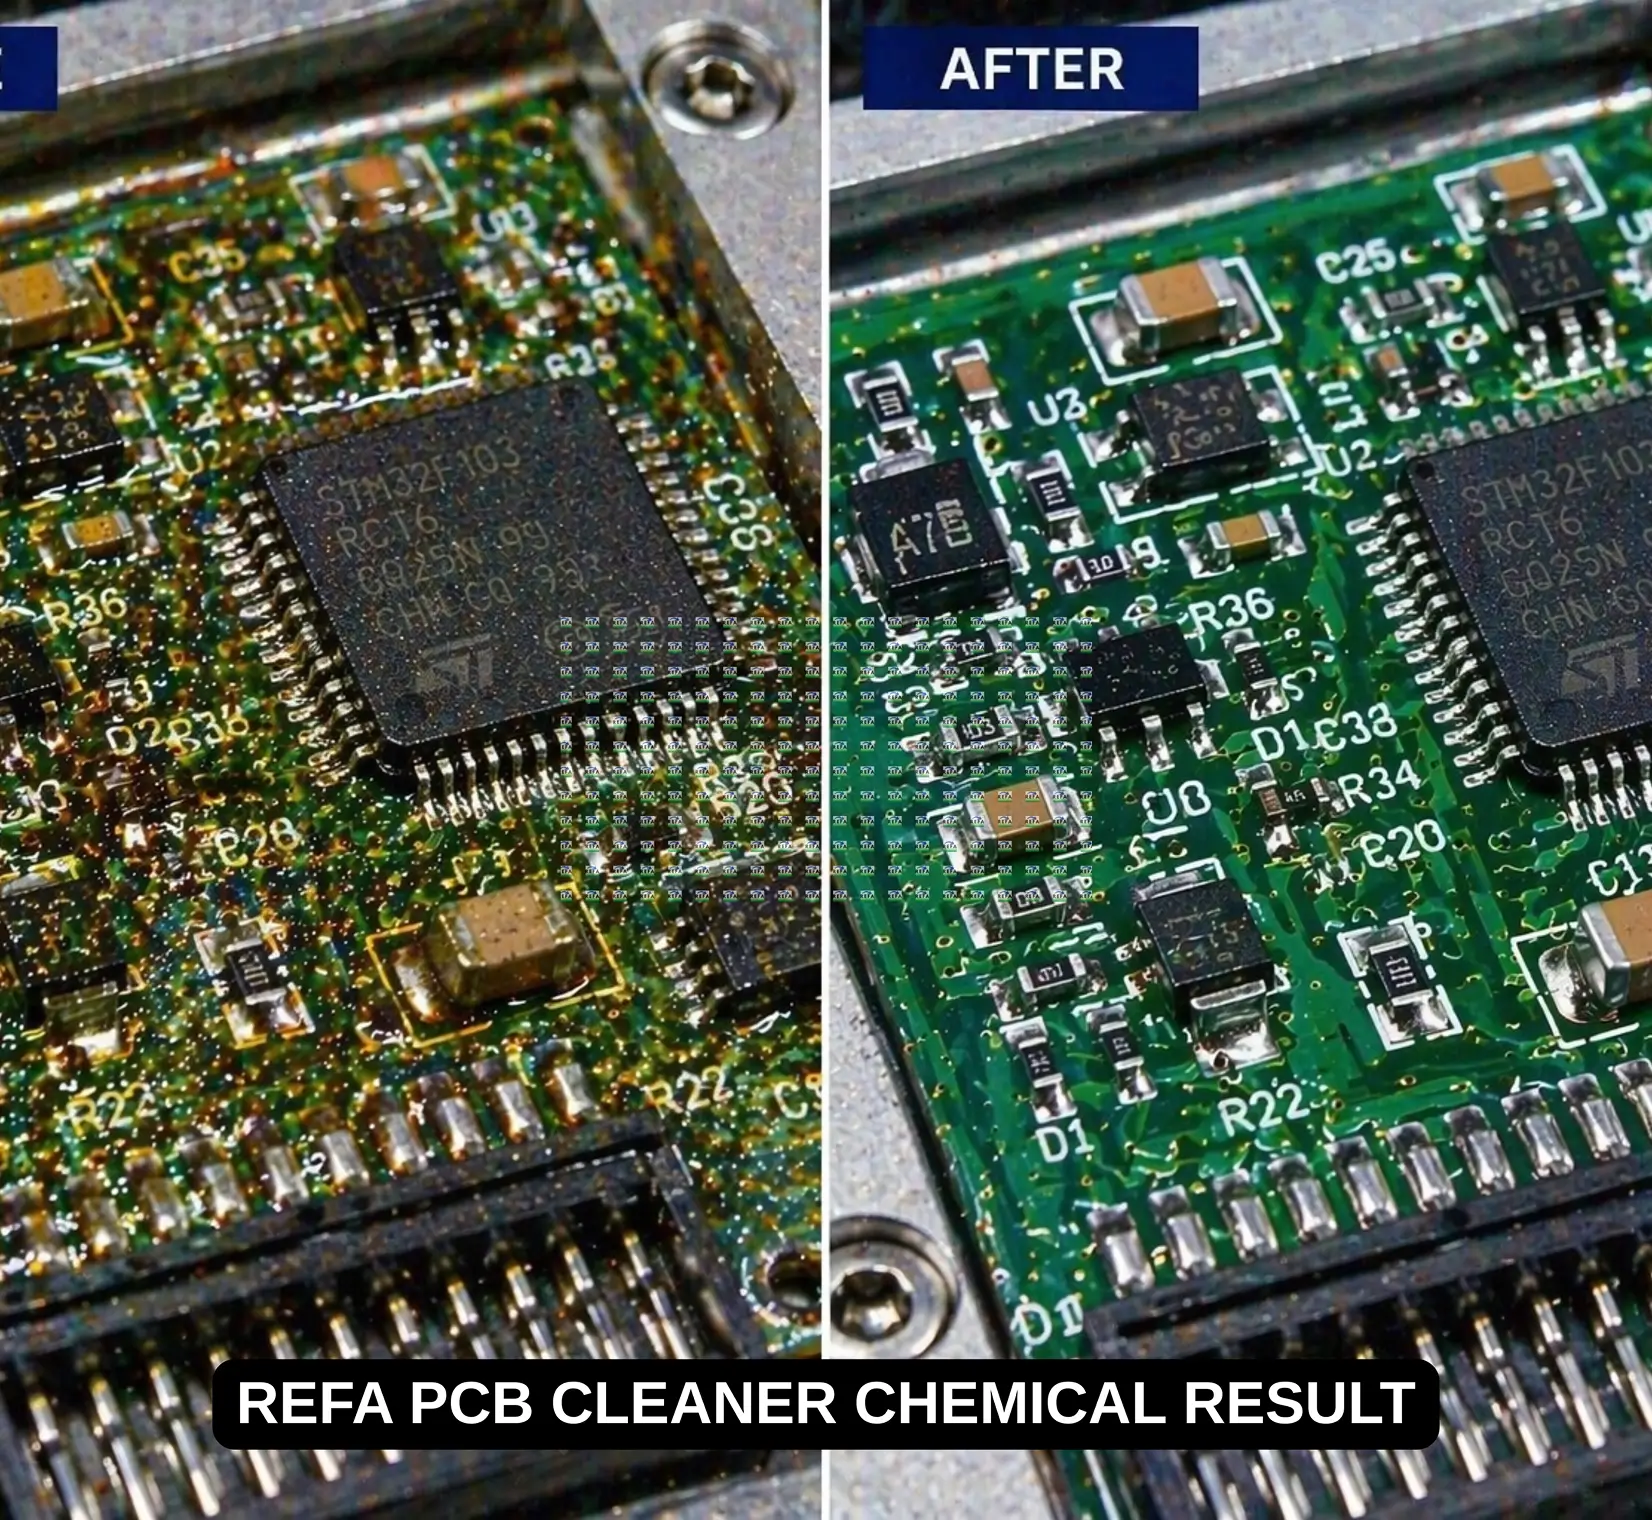
REFA Chemical Industries Pvt. Ltd., based in Greater Noida, Uttar Pradesh, manufactures water-based specialty industrial chemicals for metal cleaning, degreasing, surface preparation, metalworking, corrosion protection and related industrial applications.
For businesses searching for pan India industrial chemical supply and export, REFA offers a manufacturing-led approach to domestic supply and international sourcing enquiries, with technical product selection and application-specific support.
Why Pan India Industrial Chemical Supply Matters
India’s manufacturing sector is spread across numerous industrial regions.
Automotive component manufacturers operate in Gurugram, Manesar, Pune, Chennai, Hosur and other locations. Aluminium processors, engineering workshops, cookware manufacturers and electrical equipment producers are distributed across industrial clusters throughout the country.
Despite their geographical differences, these manufacturers often require similar chemical processes.
A machined component must be cleaned before assembly. A steel part may need rust protection during storage. A fabricated component may require pretreatment before powder coating.
However, the specific chemical requirements can vary according to material, contamination, equipment and customer specifications.
For industrial buyers, sourcing from a manufacturer capable of supporting requirements across India can offer practical advantages.
Consistent Product Specifications
When the same chemical is used at multiple manufacturing locations, consistency becomes important.
Differences in concentration, formulation or product characteristics may affect process performance.
A manufacturing-led supplier should maintain appropriate product specifications and quality controls to support repeatable production results.
Centralised Vendor Management
Companies operating several plants may prefer to evaluate a common chemical manufacturer for multiple locations.
This can simplify technical discussions, documentation, vendor approvals and commercial coordination.
However, each plant’s operating conditions should still be evaluated before adopting a common product.
Access to Application-Specific Chemicals
The nearest chemical supplier may not always offer the formulation required for a specialised application.
For example, a precision-cleaning operation may require different chemistry from an ordinary workshop degreasing process.
A wider sourcing network allows manufacturers to evaluate products based on technical suitability rather than geographical proximity alone.
Better Planning for Recurring Requirements
Industrial chemicals are often consumed continuously.
Once a product has been approved, buyers need to plan replenishment according to consumption, lead times, packaging requirements and inventory levels.
A dependable supply arrangement helps reduce the risk of production interruptions caused by chemical shortages.
REFA Chemical Industries: An Industrial Chemical Manufacturer Based in Greater Noida, India
REFA Chemical Industries Pvt. Ltd. is a specialty industrial chemical manufacturer with its manufacturing facility in Kasna Ecotech-6, Greater Noida, Uttar Pradesh.
The company’s corporate and marketing office is located in Sector 153, Noida.
REFA focuses on water-based industrial chemical formulations for manufacturing applications, including metal cleaning, degreasing, surface preparation, corrosion prevention and metalworking.
Its product categories support a range of industrial materials and processes.
Rather than approaching chemical selection purely as a commodity purchase, REFA’s application-oriented approach considers the component, contamination, equipment, process conditions and required result.
This is particularly relevant when supplying manufacturers in different regions, where the same type of component may be processed using different machinery and operating parameters.
Industrial Chemical Products Available for Domestic Supply and Export Enquiries
Industrial chemical sourcing requirements differ from one manufacturing sector to another.
REFA’s portfolio covers several major chemical categories used in metal processing and industrial production.
1. Industrial Metal Cleaning and Degreasing Chemicals
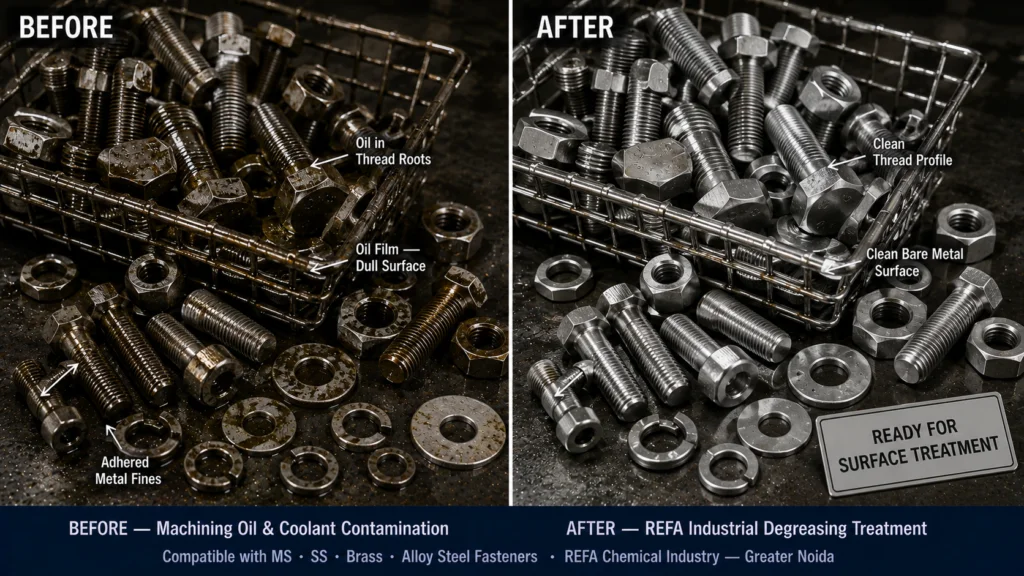
Metal cleaning chemicals remove oils, grease, machining residues and other contaminants from industrial components.
REFA’s cleaning portfolio addresses applications involving aluminium, stainless steel, mild steel, cast iron, copper, brass and selected multi-metal components.
Depending on the product and process, these chemicals may be used in immersion tanks, spray washing machines, ultrasonic cleaning equipment and other industrial washing systems.
The appropriate formulation depends on contamination type, substrate compatibility, cleaning temperature, concentration and subsequent manufacturing operations.
2. Precision and Ultrasonic Cleaning Chemicals
Precision cleaning is particularly important where residual particles, oils or other contamination can affect component performance.
Applications may include automotive HVAC components, hydraulic parts, precision-machined components and engineering assemblies.
REFA offers water-based cleaning formulations for selected precision cleaning applications.
The cleaning chemical must be evaluated as part of the complete process, including equipment, filtration, rinsing, drying and handling.
3. Metal Pretreatment and Phosphating Chemicals
Metal pretreatment prepares component surfaces for downstream processes such as painting and powder coating.
REFA’s chemical categories include iron phosphating, zinc phosphating, manganese phosphating, cleaner-cum-phosphating, surface conditioning and related pretreatment products.
These formulations require application-specific selection and process control.
4. Rust Removal and Corrosion Prevention Chemicals
Metal components may experience corrosion during manufacturing, storage or transportation.
REFA’s rust removal and preventive chemical categories support selected applications involving ferrous metals and other compatible substrates.
The appropriate product depends on the condition of the surface, required protection period, storage environment and downstream process requirements.
5. Metalworking Fluids
Machining, cutting, drawing and stamping operations require suitable lubrication and process chemistry.
REFA’s metalworking chemical categories include cutting fluids, drawing lubricants, stamping fluids and related formulations.
Product selection should account for operating conditions, material compatibility and the subsequent component cleaning process.
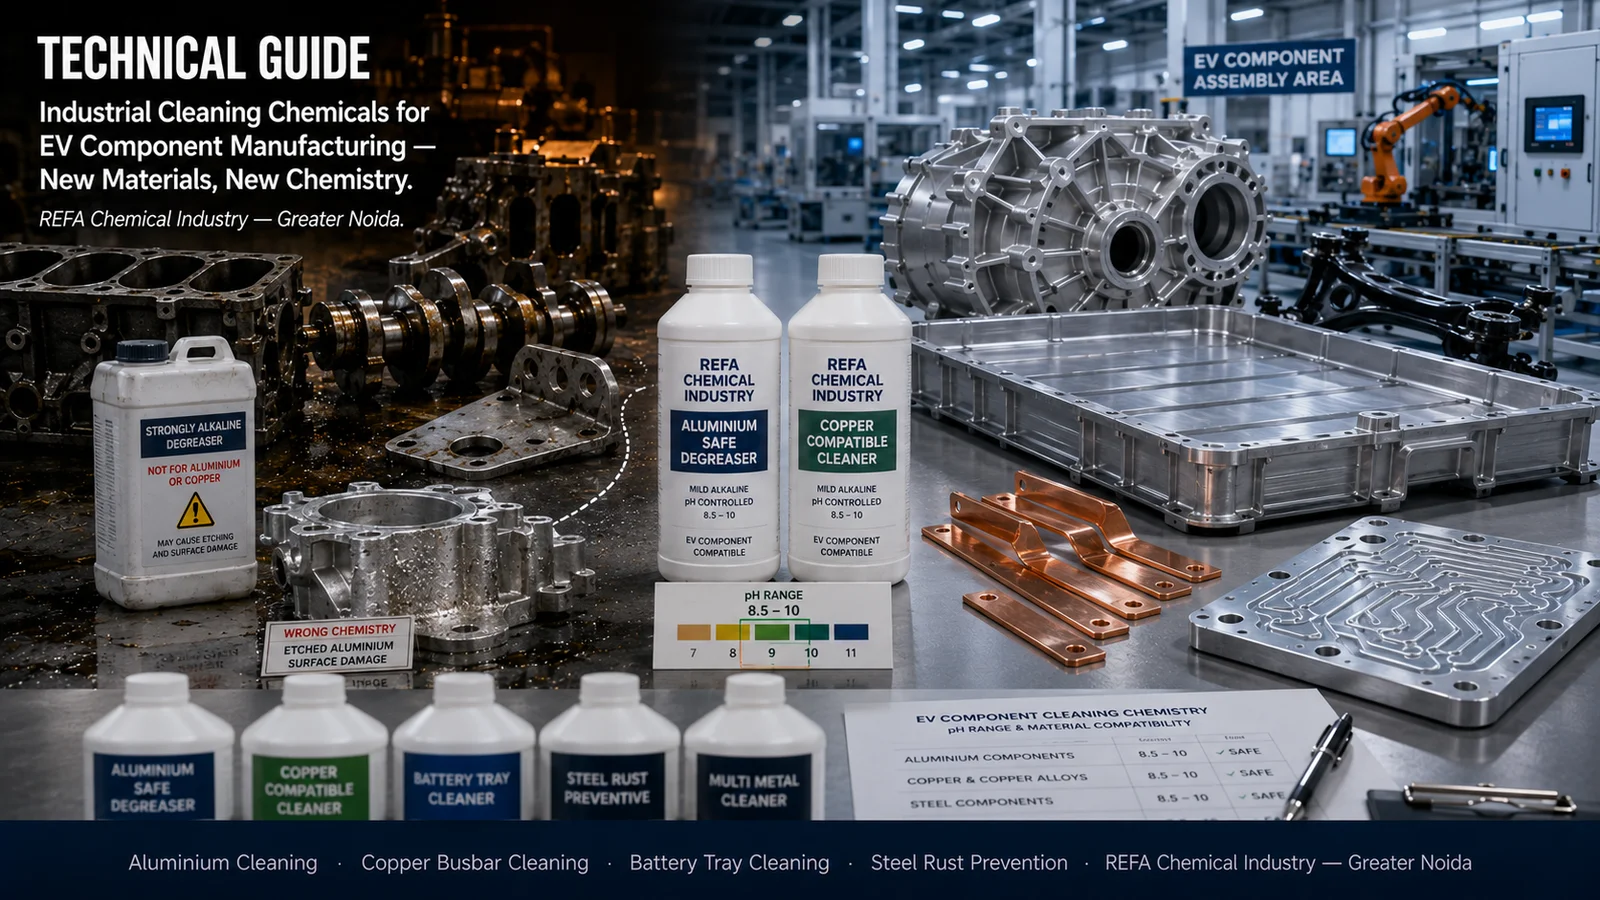
6. Aluminium Cleaning and Surface Treatment Chemicals
Aluminium processing requires careful control of chemical compatibility.
REFA’s aluminium-related product categories cover cleaning, degreasing, brightening, etching and selected surface preparation applications.
Different alloys and surface-finish requirements may require different chemical grades.
7. Industrial Maintenance and Specialty Chemicals
Manufacturing facilities also require cleaning and maintenance chemicals for machinery, industrial floors, equipment and other applications.
REFA supplies selected specialty cleaning and maintenance formulations, alongside certain industrial water treatment chemical categories.
Product availability, packaging and export suitability should be confirmed for the specific grade.
Pan India Industrial Chemical Supply: Serving Different Manufacturing Regions
India’s industrial landscape includes manufacturing clusters with distinct chemical requirements.
A supplier serving customers across India must understand these differences rather than assuming that one formulation is suitable for every factory.
Delhi NCR, Haryana and Western Uttar Pradesh
Greater Noida, Noida, Ghaziabad, Faridabad, Gurugram and Manesar contain substantial automotive component, engineering, electrical and metal fabrication activity.
Common chemical requirements include metal degreasing, component cleaning, phosphating, rust prevention and metalworking fluids.
REFA’s Greater Noida manufacturing location provides a base for serving customers in this region.
Maharashtra
Manufacturing centres such as Pune, Chakan, Talegaon, Nashik and Aurangabad have automotive, engineering and metal-processing industries.
These industries may require machining fluids, component cleaning chemicals, corrosion preventives and pretreatment formulations.
Tamil Nadu
Chennai, Sriperumbudur, Oragadam, Hosur and Coimbatore are important centres for automotive, engineering and other manufacturing activities.
Industrial chemical requirements can include precision cleaning, metal degreasing, surface treatment and metalworking fluids.
Karnataka
Bengaluru and surrounding manufacturing regions support automotive components, precision engineering, electrical equipment and other industries.
Such applications may require specialised cleaning, metalworking and surface preparation chemicals.
Gujarat
Industrial centres such as Ahmedabad, Vadodara, Rajkot and other manufacturing clusters support metal fabrication, engineering and diverse industrial production.
Chemical requirements vary according to material, equipment and manufacturing process.
Madhya Pradesh, Rajasthan and Punjab
Industrial regions including Indore, Pithampur, Dewas, Bhiwadi, Neemrana, Ludhiana and other manufacturing centres contain engineering, automotive component and metalworking businesses.
These industries can require industrial cleaners, degreasers, rust preventives, phosphating chemicals and machining fluids.
REFA welcomes industrial chemical supply enquiries from manufacturing businesses across India. Delivery feasibility, lead times, packaging and commercial arrangements are confirmed according to product and destination.
Industrial Chemical Export From India: What International Buyers Should Look For
International sourcing involves more than identifying a manufacturer with a competitive quotation.
An overseas buyer must evaluate whether the chemical is technically suitable, whether documentation is complete and whether the product can be transported and imported in compliance with applicable regulations.
For industrial chemicals, these considerations are especially important.
A cleaner that performs well in an Indian factory may require further evaluation when used with different water quality, equipment, temperatures or operating practices overseas.
Similarly, packaging and labelling requirements can vary between countries.
International buyers should therefore approach chemical sourcing as a technical and commercial qualification process.
Technical Product Evaluation
Before purchasing industrial chemicals from India, importers and end users should share information about their intended applications.
For a metal cleaning chemical, this may include:
- Component material and alloy
- Type of oil, grease or contamination
- Cleaning equipment and process
- Operating temperature and cleaning time
- Required cleanliness or surface condition
- Rinsing and drying arrangements
- Existing chemical and current operating problems
These details help determine whether an existing formulation may be suitable or whether further testing is needed.
Safety Data Sheets and Technical Data Sheets
International buyers should request product-specific Safety Data Sheets and Technical Data Sheets.
The SDS communicates relevant hazard, handling, storage, transport and emergency information.
The TDS generally provides product characteristics and recommended application guidance.
Additional declarations, test reports or country-specific documentation may be required depending on the destination and chemical.
Packaging and Transportation
Industrial chemicals may be supplied in different commercial packaging formats depending on the product, order quantity and shipping requirements.
Packaging must be compatible with the chemical and appropriate for the intended transportation conditions.
Some chemicals may be subject to dangerous goods transport rules. Classification must be determined from the actual formulation and applicable regulations.
Import Regulations
Chemical import requirements differ by country.
Buyers should confirm relevant tariff classification, customs documentation, chemical registration or notification obligations, labelling requirements and any restrictions applicable to the product.
A product being manufactured and sold in India does not automatically mean it can be imported into every overseas market without additional compliance steps.
REFA’s International Market Development
India’s specialty chemical manufacturing industry has opportunities to serve overseas manufacturers seeking technically suitable alternatives and additional sourcing options.
REFA is pursuing international business development, including engagement with prospective industrial customers and distribution partners.
Indonesia is among the markets where REFA has explored industrial chemical supply opportunities, particularly for metal cleaning, degreasing and surface treatment applications.
The company has also engaged in international manufacturing and business-development discussions involving European markets.
These activities reflect REFA’s international growth ambitions.
However, potential customers should distinguish between an export enquiry, an ongoing technical evaluation, an appointed distributor and an established commercial supply relationship.
For each destination, REFA can discuss product suitability, documentation, sampling, minimum order quantities, commercial terms and shipment feasibility.
Direct Export or Local Distributor: Which Model Works Better?
International industrial chemical supply can operate through different commercial models.
The most appropriate arrangement depends on the product, customer requirements, order volumes and local market conditions.
Direct Supply to Industrial End Users
Under this model, an overseas manufacturer purchases directly from the Indian chemical manufacturer.
Direct supply may be suitable where the customer has sufficient import capability and predictable consumption.
However, international freight, customs clearance, local storage and inventory planning must be considered.
Supply Through Importers and Distributors
A local distributor imports chemicals and supplies industrial customers in its territory.
This arrangement may offer advantages where customers prefer domestic invoicing, smaller quantities or locally available inventory.
A capable distributor may also support customer visits, trials and routine commercial coordination.
Stockist and Local Technical Sales Model
In some markets, an importer or stockist may handle local inventory while the chemical manufacturer or its representative supports technical sales and customer development.
This can combine local product availability with application-focused selling.
Each arrangement requires clear responsibilities for import compliance, inventory, technical support, commercial terms and customer service.
Why Water-Based Industrial Chemicals Can Be Relevant for Export Markets
Industrial customers in different countries may have varying safety, environmental and process requirements.
Water-based cleaning formulations can be attractive for certain applications where buyers wish to reduce dependence on particular solvent-based systems.
However, the environmental performance of a chemical depends on its actual composition and use.
Water-based does not automatically mean non-hazardous, biodegradable or compliant with every destination country’s chemical regulations.
REFA’s water-based formulation focus provides a starting point for technical evaluation, but product-specific claims should be supported by appropriate documentation.
How REFA Approaches Industrial Chemical Selection
A successful industrial chemical supply relationship begins with understanding the customer’s process.
Consider a factory that needs to remove machining oil from aluminium components.
Simply requesting an aluminium cleaner is not enough.
The manufacturer should ideally provide information about the alloy, oil type, component geometry, cleaning machine, temperature and required surface condition.
If the factory operates an ultrasonic cleaner, the selected formulation must be suitable for ultrasonic operation and the intended cleaning process.
If the components will subsequently undergo coating or anodizing, residue control and surface compatibility become particularly important.
REFA’s application-oriented approach focuses on identifying suitable formulations for evaluation rather than assuming that one chemical can solve every cleaning problem.
The same principle applies to domestic customers and international buyers.
What Makes a Reliable Pan India Industrial Chemical Supplier?
Industrial buyers should evaluate several factors before selecting a long-term chemical manufacturer.
Manufacturing Capability
Confirm whether the company manufactures the relevant products and has suitable quality-control arrangements.
Technical Understanding
The supplier should be able to discuss material compatibility, contamination, process parameters and application limitations.
Product Documentation
Relevant SDS, TDS and applicable compliance documents should be available for review.
Consistent Supply Planning
Discuss recurring requirements, production lead times, packaging, dispatch arrangements and minimum order quantities.
Trial and Evaluation Support
Where necessary, assess the chemical on actual components and under realistic operating conditions before full-scale adoption.
Commercial Transparency
Domestic and export buyers should clarify pricing basis, taxes, freight, payment terms and responsibilities.
For exports, agreed Incoterms should be clearly identified where applicable.
Long-Term Technical Support
A supplier should be willing to investigate changes in process performance, contamination, operating conditions and chemical consumption.
Frequently Asked Questions
1. Which company offers pan India industrial chemical supply and export?
REFA Chemical Industries Pvt. Ltd. is a Greater Noida-based manufacturer of water-based specialty industrial chemicals that serves domestic industrial customers and handles international sourcing enquiries. Product availability, delivery arrangements and export feasibility depend on the destination and specific chemical grade.
2. Where is REFA Chemical Industries located in India?
REFA’s manufacturing facility is located at Industrial Plot No. A-94, Kasna Ecotech-6, Greater Noida, Uttar Pradesh – 201316. Its corporate and marketing office is in Sector 153, Noida.
3. What industrial chemicals does REFA manufacture?
REFA manufactures metal cleaning and degreasing chemicals, precision cleaning formulations, phosphating and pretreatment chemicals, rust removers, corrosion preventives, metalworking fluids and selected industrial maintenance and water treatment chemicals.
4. Does REFA supply industrial chemicals across India?
REFA serves industrial customers beyond its Greater Noida manufacturing location and welcomes supply enquiries from manufacturing businesses throughout India. Delivery terms, availability and lead times are confirmed according to the product and destination.
5. Can international companies import industrial chemicals from REFA?
International manufacturers, importers and distributors can approach REFA for industrial chemical sourcing discussions. Export feasibility depends on product classification, destination regulations, commercial terms, documentation and shipping arrangements.
6. Does REFA manufacture water-based industrial cleaning chemicals?
Yes. REFA focuses on water-based specialty industrial formulations, including metal cleaners, degreasers and surface preparation chemicals.
7. Can REFA provide SDS and TDS documents for export enquiries?
Product-specific Safety Data Sheets and Technical Data Sheets can be requested as part of technical and commercial evaluation. Destination-specific documentation requirements should be confirmed before shipment.
8. Does REFA work with overseas chemical distributors?
REFA is exploring international distribution and supply relationships. Prospective importers and distributors can contact the company to discuss product categories, territory, market development and commercial arrangements.
9. Can REFA customise industrial chemicals for overseas customers?
REFA supports application-oriented formulation development. The feasibility of a customised chemical depends on the technical requirements, testing, applicable regulations and commercial considerations.
10. How can an overseas buyer request a quotation from REFA?
International buyers can contact REFA with the product application, intended quantity, destination country, packaging requirements and relevant technical specifications. The company can then discuss product selection, documentation, sampling and commercial feasibility.
Looking for a Reliable Industrial Chemical Manufacturer in India?
Whether you operate an automotive component plant in Pune, an engineering facility in Chennai, an aluminium processing unit in Gujarat or an industrial manufacturing business overseas, choosing the right chemical manufacturer is an important operational decision.
REFA Chemical Industries Pvt. Ltd. manufactures water-based specialty industrial chemicals for metal cleaning, degreasing, surface preparation, metalworking and related manufacturing applications.
We welcome enquiries from Indian industrial manufacturers, international end users, chemical importers and distribution partners.
Share your application, product requirements, estimated consumption and delivery location with our team to begin a technical and commercial discussion.
REFA Chemical Industries Pvt. Ltd.
Manufacturing Unit: Industrial Plot No. A-94, Kasna Ecotech-6, Greater Noida, Uttar Pradesh – 201316, India
Corporate & Marketing Office: Sector 153, Noida, Uttar Pradesh, India
Email: info@refachemical.com
Website: https://refachemical.com/
REFA — Research Engineered Formulations & Applications.